How a Thermocol Packaging Manufacturer Cut Tool Breakage by 95% and Pattern Costs by 50% with 3D Printing


Every foundry owner knows the feeling.
You’ve just finished a casting run, and the VMC operator walks in with a broken tool in his hand. Again. The fourth one this month. And the root cause is always the same: the pattern wasn’t accurate enough.
This is the story of how Ganga Thermopack solved that problem for good, with a GO3D BX 700 and a roll of PLA Pro filament. A year later, they run four GO3D printers.
At a Glance
| Customer | Ganga Thermopack, thermocol packaging moulds and tooling |
|---|---|
| Application | 3D printed patterns for aluminium sand casting |
| Machines | GO3D BX 700 (July 2025), then a GO3D B 700 added (March 2026), then two more GO3D printers |
| Build volume | 700 × 500 × 500 mm |
| Material | PLA Pro, PETG Pro for selected patterns |
| Pattern life | 30 to 40 castings per pattern |
| Tool breakage | 95% lower (4 to 5 tools per job down to near zero) |
| Pattern cost | About 50% lower than wooden patterns |
| Savings | ₹72,000 a month, ₹8.6 lakh a year |
Who Is Ganga Thermopack?
Ganga Thermopack is a manufacturer of precision thermocol packaging and tooling. Their moulds are used in packaging for coolers, washing machines and consumer appliances. Their work demands accuracy: the packaging moulds they produce must match exact dimensions, and the aluminium castings that form those moulds must come out right every time.
For years, pattern making was their biggest operational headache.
The Problem: Wooden and Thermocol Patterns Were Destroying Productivity
Before GO3D, Ganga Thermopack used two types of patterns for their aluminium casting process: wooden patterns and thermocol patterns. Both created serious problems.
Wooden Patterns
Wooden patterns are the traditional choice for sand casting. The problem is that wood warps, shrinks and is hand crafted, so dimensional consistency from one pattern to the next is never guaranteed.
At Ganga Thermopack, this showed up as:
- Dimensional inaccuracies: patterns deviated from the CAD design, leading to unpredictable casting dimensions
- Uncontrolled machining margins: excess material stock remained on cast parts, forcing VMC operators to remove more material than planned
- Frequent tool breakage: when the casting dimensions were off, cutting tools hit unexpected material and snapped
Thermocol Patterns
Thermocol was cheaper and faster to make, but even less reliable.
- Pattern distortion and bending: the soft material deformed during sand compaction, producing warped or bent castings
- Severe tool breakage: approximately 4 to 5 expensive cutting tools broken per job, traced to dimensional errors from the thermocol patterns
- Production downtime: each broken tool meant stopping the VMC machine, replacing the tool, resetting the program, and restarting
The financial impact was significant. Beyond the direct cost of broken tools, every stoppage meant delayed deliveries and overtime. The root cause, pattern inaccuracy, was never fixed, only managed.
The Solution: FDM 3D Printing on Site with the GO3D BX 700
Ganga Thermopack installed a GO3D BX 700, an industrial FDM 3D printer with a 700 × 500 × 500 mm build volume, specifically to replace their pattern making process.
The material of choice: PLA Pro. It is cost effective, dimensionally stable and rigid enough for repeated sand casting. For some patterns they use PETG Pro.

A 3D printed PLA Pro pattern produced on the GO3D BX 700. The hollow cavity is formed by the printing, eliminating excess machining margins.
How the New Workflow Works
The transition simplified their whole process into one flow:
CAD Design → 3D Print (GO3D BX 700) → Sand Casting → VMC Machining
A single designer now manages the entire workflow from start to finish: designing the pattern in CAD, sending it to the BX 700, supervising the print, and generating the VMC machining program for the finished casting. No external pattern vendor. No dependence on a skilled pattern maker. No waiting.

Complex curved geometries that would distort in thermocol patterns are produced consistently in 3D printed PLA Pro.
Print Settings That Work
Through production experience, Ganga Thermopack’s team developed a set of settings for casting patterns:
| Parameter | Setting |
|---|---|
| Nozzle size | 0.6 mm |
| Layer height | 0.4 mm |
| Wall count | 3 walls |
| Infill density | 8% |
| Material | PLA Pro (PETG Pro for selected patterns) |
These settings give fast print times without hurting pattern usability. The layer lines from a 0.4 mm layer height do not affect the cast surface, so no sanding is needed before use. Each pattern produced at these settings is durable enough for 30 to 40 aluminium castings before it needs replacing.
Best Practices Learned on the Shop Floor
Three practices emerged from production:
1. Draft angles are non-negotiable. Build enough draft into the CAD design before printing. Correct draft angles let the pattern come out of the sand mould cleanly, giving better surface finish and higher casting success rates.
2. Print large patterns as a single piece. Multi part assemblies glued together risk differential shrinkage, and the pattern bends at the joint. Where the build volume allows, printing one piece removes this risk.
3. Use a 0.6 mm nozzle for large patterns. The larger nozzle deposits more material per pass, and cuts print time on large patterns, with no meaningful loss in surface quality for casting.
The Results: Three Numbers That Tell the Story

The finished aluminium cast part sitting inside its 3D printed PLA Pro pattern, dimensionally accurate and ready for VMC machining.
95% Reduction in Tool Breakage
The most dramatic result. Tool breakage dropped from 4 to 5 tools broken per job to near zero. In the worst case encountered since switching to 3D printed patterns: one tool. The root cause, dimensional inaccuracy in the pattern, is gone. Castings now align closely with the CAD model and VMC operations run smoothly.
50% Lower Pattern Costs
Making patterns on site removed outsourcing costs. The PLA Pro filament in a pattern costs a fraction of what Ganga Thermopack paid external pattern vendors, or spent on materials and skilled labour for wooden patterns. Against wooden patterns, cost per pattern dropped by about 50%.
1 Person. Start to Finish.
The most significant operational change. What previously required a skilled pattern maker (or an outside vendor), a casting specialist and a VMC programmer is now managed by one designer. CAD, print, machining program. Fewer handoffs, fewer delays, fewer miscommunications.
“3D printed patterns are highly accurate and consistent. Tool breakage reduced from 4 to 5 per job to mostly zero. Our machining operations are now smooth, with big savings in cutting tool cost and reduced machine downtime.”
Keshav Singhal, Product Head, Ganga Thermopack
ROI in Practice: What It Adds Up To
| Item | Calculation | Saving |
|---|---|---|
| Pattern cost | ₹25,000 outsourced pattern vs ₹10,000 printed, 4 patterns a month | ₹60,000 a month |
| Cutting tools | ₹750 per tool, 4 tools a job, 4 jobs a month | ₹12,000 a month |
| Total | ₹72,000 a month | |
| Per year | ₹8.6 lakh | |
| Over 5 years | ₹40 lakh+ |
Ganga Thermopack uses 4 to 6 patterns a month. The figures above use the low end, so they are conservative. Machine downtime savings are not included. Tool savings run ₹1,000 to ₹5,000 per job.
One Printer to Four
The success of the first machine led Ganga Thermopack to add a second: the GO3D B 700.
The B 700 has the same 700 × 500 × 500 mm build volume with faster print speed. A reference part that took about 3 days on the BX 700 prints in about 1.5 days on the B 700. That is 2× throughput with no change in quality.
Running both machines, Ganga Thermopack can print in parallel: one machine printing while the other’s output is cast and machined. Since then they have added two more GO3D printers, taking their fleet from one printer to four within a year.
The Production Cycle in Photos
Three real production examples from Ganga Thermopack’s workflow, each going from 3D printed pattern, to as-cast aluminium part, to VMC machined final component:

An as-cast aluminium part produced using a 3D printed PLA Pro pattern. The cavity is clean and accurate, reproduced from the CAD design.

Close-up of a finished cast part. Dimensional accuracy from the 3D printed pattern means VMC operators have predictable machining margins, removing the unexpected load events that previously caused tool breakage.

Circular patterns with internal cavities, geometries that are particularly difficult in wooden or thermocol pattern making, are produced reliably on the BX 700 and B 700.
Is This Right for Your Foundry?
The Ganga Thermopack workflow is directly applicable to any foundry that:
- Faces dimensional variation: inconsistent castings from wooden or thermocol patterns
- Suffers high tool breakage: 2 or more tools broken per job due to uncontrolled machining margins
- Experiences pattern distortion: bending or warping common in thermocol patterns
- Wants faster iterations: needs to change a dimension or add a vent or gate without building a new pattern from scratch
- Depends on external vendors: wants pattern production on site and control over lead times
Planning patterns for your own foundry? See how GO3D 3D printers work for foundry casting patterns. Or explore all 3D printing applications.
If any of these match your operation, the ROI calculation is straightforward: compare your monthly tool replacement cost plus pattern vendor spend against the cost of a GO3D BX 700. Most foundries in Rajkot, Coimbatore, Kolhapur, and Belgaum recover the machine cost within 8 to 14 months.
Technical Specifications: GO3D BX 700
| Specification | Detail |
|---|---|
| Build volume | 700 × 500 × 500 mm |
| Technology | FDM / FFF |
| Compatible materials | PLA, PLA Pro, PETG, ABS, ASA, PLA-CF |
| Nozzle options | 0.4 mm, 0.6 mm, 0.8 mm |
| Manufacturer | GO3D Innovation LLP, Kuha, Ahmedabad, India |
| Certification | Make in India |
| Support | Pan India, 24 to 48 hour response |
Talk to GO3D About Your Foundry
GO3D Innovation LLP manufactures industrial 3D printers in Kuha, Ahmedabad, Gujarat. Our BX series, the BX 700 and BX 1200, is built for industrial pattern making, large format prototyping and production.
We work directly with foundries across Rajkot, Coimbatore, Kolhapur, Belgaum, Batala and Pune, and we understand casting applications in detail. Call +91 90549 83700, email sales@go3d.in or use our contact page.
Frequently Asked Questions
Can PLA Pro patterns withstand repeated aluminium casting?
Yes. At the print settings used by Ganga Thermopack (3 walls, 8% infill, 0.4 mm layer height), PLA Pro patterns consistently last 30 to 40 casting cycles before showing wear. For longer-running patterns, PETG or PLA-CF can extend this further.
Do the layer lines from 3D printing affect the cast surface finish?
At 0.4 mm layer height with a 0.6 mm nozzle, layer lines are generally not visible in the final aluminium casting surface. Ganga Thermopack’s team reports no sanding is required before use in their application. For applications requiring very fine surface finish, a light sand or coating may be applied.
What’s the minimum build volume needed for pattern making?
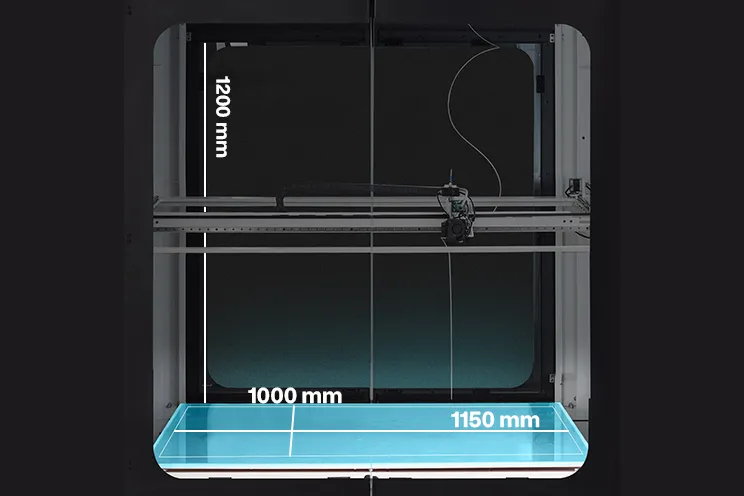
It depends on your largest pattern. The BX 700 (700 × 500 × 500 mm) handles most standard casting patterns. For very large patterns, such as washing machine body moulds, the BX 1200 (1150 × 1000 × 1200 mm) is the appropriate machine.
Can we print patterns for investment casting, not just sand casting?
Yes. For investment casting, castable PLA or wax-blend filaments are used instead of standard PLA Pro. The workflow is identical, and the material burns out cleanly during the casting process.
How long does it take to train an operator?
Ganga Thermopack’s designer was operating the machine independently within 2 to 3 days of installation. GO3D provides full onsite training and remote support.
Do you provide support in Rajkot / Coimbatore / Kolhapur?
Yes. GO3D has a pan India service network with a target response time of 24–48 hours for all locations.
Case study data sourced from Ganga Thermopack customer interview, March 2026. GO3D Innovation LLP, Kuha, Ahmedabad, Gujarat, India.


Let’s set the ball rolling with your next project
Get in touch with our team
